Of all the parameters to keep under control in production, the melting temperature of polyurethane glue is one of those that seem obvious — until something goes wrong.
Working out whether it’s set correctly isn’t just a matter of reading the technical data sheet and the numbers on the operator panel: it also needs to be verified directly.
Where to start: the type of application system
The melting temperature should be set on the operator panel according to the type of glue used and the application system — which may be a coating head or a roller coater — following the values indicated in the technical data sheet.
The check doesn’t end at the operator panel
Setting the value indicated in the technical data sheet (TDS) to achieve the desired degree of viscosity isn’t enough on its own, however.
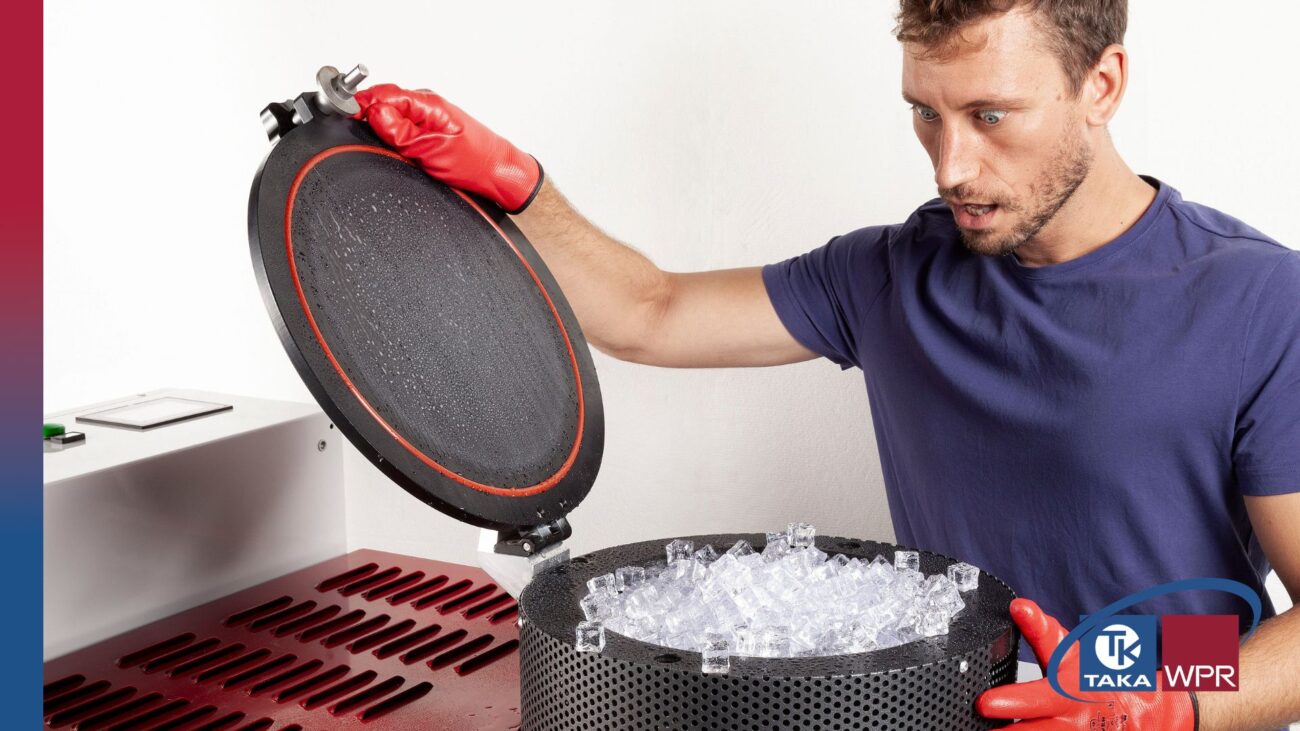
To be sure the glue really is at the correct temperature, a periodic check with an IR thermometer and/or a probe thermometer is needed, and the point at which to measure changes depending on the system:
- with the roller coater, the measurement can be taken directly on the glue between the applicator roller and the metering roller;
- with the glue head, the check should be carried out directly on the glue inside the melter, preferably with a probe thermometer.
What happens if the glue is too hot
An HMPUR glue kept at an excessively high temperature can create concrete problems for the process. In both cases, the main risk is that of “burning the glue” — that is, progressively compromising its stability within the melting system.
In an initial phase, exposure to excessively high temperatures can cause an increase in the glue’s viscosity. This phenomenon tends to intensify over time, progressively reducing the mobility of the material within the melting system. The increase in viscosity is linked to the chemical curing process of the HMPUR, which can be affected both by temperature and by the moisture present inside the melter. High temperatures and the presence of moisture can in fact accelerate the reaction, encouraging a progressive change in the characteristics of the adhesive.
As the glue becomes less mobile, it tends to remain longer in certain areas of the system, where it can be subjected to high temperatures for ever-longer periods. This creates a vicious circle: the increase in viscosity reduces the mobility of the glue, the longer dwell time further encourages degradation, and the material progressively tends to deteriorate, until it reaches so-called “burnt glue.”
The presence of degraded glue within the system has a negative impact on the performance of the melting system, increasing the risk of process anomalies, build-ups and contamination. As a result, the system may require increasingly frequent maintenance, with a consequent rise in downtime and operating costs.
In summary
The correct melting temperature of the glue starts from a correct setting on the operator panel but is only confirmed with a direct check depending on the system used.
A temperature that’s too high is no minor detail: it can compromise the stability of the glue itself within the melting system.
The TAKA-WPR Academy gives you the opportunity to train your operators on the importance of application parameters and how to measure them directly on your own lamination line.